](https://kaishanpro.com/wp-content/uploads/2026/10/What-is-a-regenerative-adsorption-dryer.webp)
Moisture in compressed air can cause corrosion, frozen pipelines, damaged pneumatic equipment, and product contamination. Standard drying methods may not provide sufficiently low dew points.
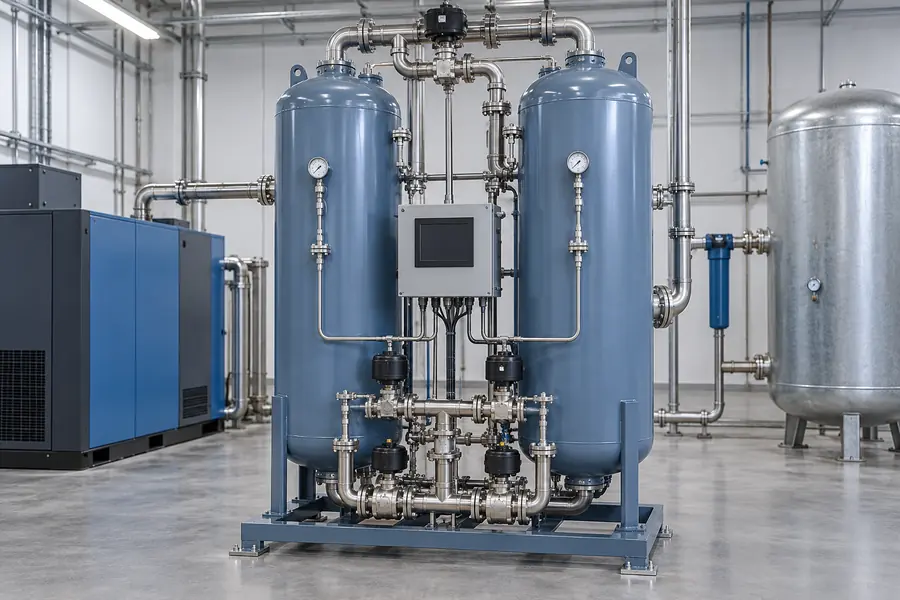
A regenerative adsorption dryer is a compressed-air drying system that removes water vapor using a moisture-adsorbing material called desiccant. Most designs use two towers: one dries the compressed air while the other regenerates its saturated desiccant. By alternating between adsorption and regeneration, the dryer continuously supplies dry compressed air, commonly at pressure dew points of −20°C or −40°C.
Evaluate adsorption dryers by working principle, regeneration method, dew point, purge consumption, installation, and operating costs to ensure efficient performance without unnecessary expenses or overinvestment.
What Is a Regenerative Adsorption Dryer and How Does It Work?
A regenerative adsorption dryer removes water vapor from compressed air through a physical adsorption process. Its regeneration system allows the drying material to be reused through repeated operating cycles.
Most regenerative adsorption dryers contain two desiccant-filled vessels, switching valves, regeneration equipment, and a controller. Wet compressed air passes through one vessel, where moisture adheres to the desiccant. Meanwhile, the other vessel releases previously collected moisture through a regeneration process. The vessels periodically exchange functions to maintain continuous drying.
What does adsorption mean?
Adsorption is a physical process in which water-vapor molecules attach to the surface of a material.
In compressed-air dryers, that material is called:
desiccant.
Common desiccants include:
- Activated alumina
- Silica gel
- Molecular sieves
- Specialized structured desiccant materials
The desiccant has a large internal surface area that can capture water vapor.
The basic process is:
Wet compressed air → desiccant bed → water vapor adsorbed → dry compressed air
As the process continues, the desiccant gradually approaches its moisture-holding capacity.
It must then be regenerated.
What does regeneration mean?
Regeneration is the process of removing moisture from the saturated desiccant.
Instead of throwing the desiccant away after one drying cycle, the dryer restores its adsorption capacity.
This normally involves:
reducing pressure
using dry purge air
applying heat
or:
using a combination of these methods.
After regeneration, the desiccant can be used for another drying cycle.
This is what makes the equipment a regenerative adsorption dryer.
How does a twin-tower adsorption dryer work?
A typical twin-tower system operates through four stages.
Stage 1: Adsorption
Wet compressed air enters Tower A.
The air passes through the desiccant, which captures water vapor.
Dry compressed air flows toward the distribution system.
At the same time, Tower B is isolated from the main compressed-air flow.
Stage 2: Regeneration
Tower B undergoes regeneration.
Depending on the dryer design, dry purge air, heated air, or another regeneration method removes moisture from its desiccant.
The moisture-laden regeneration air is discharged through the designated exhaust system.
Stage 3: Repressurization and preparation
Before the regenerated tower returns to normal drying service, it must be prepared for the next adsorption cycle.
For many twin-tower systems, this includes repressurization.
Heated dryers may also require a cooling stage before changeover.
Stage 4: Tower switching
The control system switches the towers.
Tower B begins drying compressed air.
Tower A starts its regeneration cycle.
The process repeats automatically.
The operating sequence can be summarized as:
Tower A: Adsorption | Tower B: Regeneration
↓
Tower A: Regeneration | Tower B: Adsorption
This arrangement allows the dryer to provide a continuous supply of dry air.
What is the difference between adsorption and absorption?
These terms are often confused.
Adsorption means moisture attaches to the surface of a drying material.
Absorption means moisture enters the bulk of another material.
In industrial compressed-air systems, regenerative desiccant dryers use adsorption.
Their desiccant can be regenerated and reused through many cycles.
By contrast, certain absorption-based drying materials are progressively consumed and need replenishment.
Atlas Copco explains the distinction in its technical guide, How an Adsorption Dryer Works.
What are the main components?
| Component | Main function |
|---|---|
| Adsorption towers | Contain desiccant and alternate between drying and regeneration |
| Desiccant | Adsorbs water vapor |
| Inlet switching valves | Direct wet air to the active tower |
| Outlet/check valves | Direct dry air toward distribution |
| Regeneration system | Removes moisture from the saturated desiccant |
| Purge valves and orifices | Control regeneration airflow where used |
| Exhaust valves and mufflers | Release moisture-laden regeneration air |
| Heater or blower | Supplies regeneration energy on applicable designs |
| Controller | Manages cycle timing and switching |
| Dew point sensor | Monitors outlet moisture performance |
| Prefilters | Protect desiccant against liquid and oil contamination |
| Afterfilter | Captures desiccant dust where required |
I consider the switching valves and regeneration system just as important as the desiccant itself.
A dryer with good desiccant can still produce a high dew point if its regeneration cycle fails.
What Are the Different Types of Regenerative Adsorption Dryers?
Regenerative adsorption dryers are mainly classified by how they remove moisture from the saturated desiccant. The regeneration method strongly influences energy consumption and operating cost.
The main types are heatless regenerative, heated purge, blower purge, and heat-of-compression dryers. Heatless systems use dry compressed air for regeneration. Heated systems add thermal energy to reduce purge demand. Blower purge systems use heated ambient air, while heat-of-compression dryers recover thermal energy from compatible compressors.
1. Heatless regenerative adsorption dryers
Best for: simpler installations and many small-to-medium airflow applications
Heatless regenerative dryers are also called:
pressure swing adsorption dryers.
They use a portion of already dried compressed air to regenerate the saturated tower.
The purge air is expanded to a lower pressure.
That very dry, low-pressure air flows through the wet desiccant and removes moisture.
The humid regeneration air then exits through the exhaust system.
A typical heatless dryer may consume approximately:
15%–20% of its rated compressed-air flow
for regeneration, depending on the design and operating conditions.
Kaeser explains that heatless dryers are usually less expensive to purchase but can be more expensive to operate because of continuous purge-air consumption.
Source: Kaeser — Desiccant Dryers.
Main advantages
Simple mechanical design, no regeneration heater, and relatively straightforward maintenance.
Main limitation
Higher compressed-air losses during regeneration.
For a factory with a large continuous air demand, this can create substantial electricity costs at the upstream compressor.
2. Heated purge adsorption dryers
Best for: industrial operations seeking lower purge-air losses
A heated purge dryer uses external heat to assist desiccant regeneration.
The regeneration process generally uses:
heated dry purge air.
Because warmer regeneration air can remove more moisture, less compressed purge air is required than with a comparable heatless design.
Kaeser's KED range, for example, uses approximately:
7% purge air
under its published operating conditions.
Source: Kaeser — Heated Purge Desiccant Dryers.
Main advantages
Lower compressed-air consumption for regeneration and potentially lower total running cost at suitable operating hours.
Main limitations
Heater electricity, additional components, and greater initial cost.
I evaluate both:
compressed-air savings + heater energy consumption.
A lower purge percentage does not automatically mean lower total electricity use under every condition.
3. Blower purge regenerative dryers
Best for: larger industrial compressed-air systems
Blower purge dryers use a blower to move ambient air through an electric heater.
The heated air then passes through the wet desiccant bed and removes accumulated moisture.
Because much of the regeneration air comes from the atmosphere rather than the compressed-air network, compressed-air purge losses can be very low.
Kaeser's KBD blower purge range is designed for approximately:
500–4,300 SCFM at 100 PSIG
with pressure dew points down to:
−40°F (−40°C).
The manufacturer describes configurations with approximately 1% or no process-air loss, depending on the operating design.
Source: Kaeser — Blower Purge Desiccant Dryers.
Main advantages
Very low compressed-air purge losses and attractive economics for certain large continuous-duty installations.
Main limitations
Higher purchase price, heater and blower energy, and more complex equipment.
Some designs use dry compressed air during cooling, while others employ alternative cooling arrangements.
I verify the full operating cycle before accepting a claim of zero purge.
4. Heat-of-compression regenerative dryers
Best for: suitable large oil-free compressor installations
Heat-of-compression, or HOC, dryers recover heat generated during air compression.
Instead of discarding this heat through cooling systems, the dryer uses it to regenerate the desiccant.
The concept is:
Compressor waste heat → desiccant regeneration → reduced additional drying energy
Atlas Copco describes HOC drying as especially suitable for compatible oil-free compressor systems with sufficient available compression heat.
HOC dryers may use:
twin-tower arrangements
or:
rotary drum systems.
Some configurations offer little or no compressed-air purge loss.
However, the achievable pressure dew point depends on the system design and available regeneration temperature.
For example, certain HOC designs commonly target approximately:
−20°C PDP
unless additional equipment is used.
I do not assume that every HOC dryer automatically achieves −40°C or −70°C.
Regeneration method comparison
| Dryer type | Regeneration method | Typical purge-air requirement | Main consideration |
|---|---|---|---|
| Heatless | Expanded dry compressed air | Approximately 15–20% | Simple design, higher air loss |
| Heated purge | Heated dry purge air | Approximately 6–8% | Lower purge, heater energy |
| Blower purge | Heated ambient air | Very low or zero on some designs | Higher capital cost, blower/heater energy |
| Heat of compression | Recovered compressor heat | Low or zero on suitable designs | Requires compatible compressor system |
Values are indicative manufacturer ranges, not universal guarantees. Rated capacity, dew point, cooling arrangement, and operating conditions change actual consumption.
My rule is:
The best regeneration method depends on annual airflow demand and the total energy required for drying.
When Should You Use a Regenerative Adsorption Dryer Instead of a Refrigerated Dryer?
Regenerative adsorption dryers are designed for applications requiring significantly drier compressed air than a typical refrigerated dryer can provide.
I recommend evaluating a regenerative adsorption dryer when the process requires a pressure dew point below 0°C, compressed-air pipelines operate in freezing environments, or sensitive production equipment requires very low moisture content. Refrigerated dryers are usually more economical when a pressure dew point around +3°C to +7°C is sufficient.
The importance of pressure dew point
Pressure dew point, or PDP, describes the temperature at which water vapor in compressed air begins to condense at the specified operating pressure.
A lower PDP means:
less water vapor remains in the compressed air.
Common targets include:
+3°C PDP
for many general industrial refrigerated-dryer applications.
−20°C PDP
for moderately low-moisture applications.
−40°C PDP
for more demanding instrument-air and industrial drying requirements.
−70°C PDP
for specialized applications requiring extremely low moisture content.
These are performance targets, not the temperature of the compressed air leaving the dryer.
A dryer delivering:
−40°C PDP
does not necessarily discharge air at −40°C.
It delivers air containing sufficiently little water vapor that condensation would begin only at that dew point under the specified pressure conditions.
ISO 8573-1 water purity classes
ISO 8573-1 defines compressed-air purity classes for:
particles
water
and:
oil.
For moisture specified by pressure dew point, common classes include:
| ISO 8573-1 water class | Maximum pressure dew point |
|---|---|
| Class 1 | −70°C |
| Class 2 | −40°C |
| Class 3 | −20°C |
| Class 4 | +3°C |
| Class 5 | +7°C |
| Class 6 | +10°C |
The applicable international standard is ISO 8573-1:2010.
Source: ISO — Compressed Air Purity Classes.
An adsorption dryer is often selected for water classes 1–3.
However, meeting a water class does not automatically guarantee compliance with the required particle or oil classes.
Those contaminants must be controlled separately.
Refrigerated dryer versus regenerative adsorption dryer
| Feature | Refrigerated dryer | Regenerative adsorption dryer |
|---|---|---|
| Main process | Cooling and condensation | Desiccant adsorption |
| Typical PDP | +3°C to +7°C | −20°C, −40°C, or −70°C |
| Best application | General industrial compressed air | Low-moisture critical applications |
| Subfreezing pipework | Often insufficient | Suitable when correctly specified |
| Desiccant required | No | Yes |
| Regeneration cycle | No | Yes |
| Purge-air loss | Generally none for regeneration | Depends on dryer type |
| Equipment complexity | Usually lower | Usually higher |
| Operating cost | Often lower for general air | Depends on regeneration technology |
| Moisture sensitivity | Moderate | High |
I do not automatically select the dryer with the lowest possible dew point.
Unnecessary over-drying can increase investment and energy consumption.
Typical applications
Outdoor compressed-air pipelines
An adsorption dryer can reduce freezing risk when the compressed-air network passes through cold environments.
The required PDP should be selected below the lowest expected downstream temperature, with an appropriate engineering margin.
Pneumatic instrumentation
Sensitive valves and instruments may require dry compressed air to prevent condensation and malfunction.
Electronics manufacturing
Dry compressed air can protect moisture-sensitive processes and equipment.
Food and beverage production
Certain processes require low moisture content to protect product quality and equipment.
However, food-contact air may need additional particle, oil, and microbiological controls.
A low dew point alone does not prove that the air is sterile or food-safe.
Pharmaceutical manufacturing
Specialized processes may require tightly controlled compressed-air purity.
The drying requirement should be based on the process specification and documented quality standards.
Chemical and industrial processing
Dry compressed air can help reduce moisture-related product and equipment problems.
Why not use a regenerative dryer everywhere?
Regenerative adsorption dryers can provide excellent air quality, but their installation may introduce:
additional pressure drop
purge-air consumption
heater electricity
desiccant maintenance
and:
higher equipment costs.
If the application only requires:
+3°C PDP
a refrigerated dryer may provide a simpler, more economical solution.
I choose dryer technology based on the required moisture limit rather than the assumption that drier air is always better.
How Do You Size, Maintain, and Troubleshoot a Regenerative Adsorption Dryer?
A regenerative dryer must be matched to the actual compressor system. Excessive flow, high inlet temperature, low operating pressure, contamination, and regeneration failures can reduce performance.
I size a regenerative adsorption dryer using required net outlet airflow, operating pressure, inlet temperature, target pressure dew point, and regeneration losses. For reliable operation, I protect the desiccant with suitable upstream separation and filtration, maintain valves and purge systems, monitor outlet dew point, and inspect the desiccant and downstream filters.
Step 1: Calculate required net airflow
The dryer must deliver enough dry compressed air to the plant.
This is especially important for heatless dryers.
Consider an illustrative example:
Dryer inlet airflow: 1,000 CFM
Regeneration purge: 15%
The purge requirement is approximately:
150 CFM.
The remaining nominal outlet flow is approximately:
850 CFM.
This example assumes the 15% purge is referenced to the same inlet flow and ignores additional losses.
The actual result depends on how the manufacturer defines dryer rated capacity.
If a factory requires:
1,000 CFM of usable dry air
a heatless dryer nominally rated at 1,000 CFM inlet may not be adequate.
I verify:
net outlet capacity
rather than only the catalogue airflow.
Step 2: Check operating pressure
Dryer performance depends on system pressure.
Lower-than-design pressure can increase volumetric flow through the dryer and reduce effective drying capacity.
I therefore specify:
normal pressure
minimum pressure
and:
maximum pressure.
All values must be compatible with the dryer design.
Step 3: Check compressed-air inlet temperature
Higher inlet temperature generally increases the moisture load on the desiccant.
A dryer designed for one inlet temperature may fail to maintain its target PDP if the actual air arrives substantially hotter.
I inspect:
compressor aftercooler
cooling system
and:
moisture separator
before increasing dryer capacity.
Step 4: Install proper upstream filtration
The desiccant is intended to remove water vapor.
It should not be exposed to excessive:
liquid water
or:
oil aerosols.
A typical arrangement is:
Compressor → aftercooler → moisture separator → appropriate prefiltration → adsorption dryer
For oil-injected compressor systems, an appropriate coalescing prefilter is especially important.
Atlas Copco specifically identifies upstream moisture separation and oil-removal filtration as essential for protecting adsorption media.
Source: Atlas Copco — Adsorption Dryer Operation.
Step 5: Protect downstream equipment
Traditional bead-type desiccant can generate dust as the media wears.
A downstream particulate afterfilter is commonly installed to capture that dust.
The complete system may become:
Compressor
↓
Aftercooler
↓
Moisture separator
↓
Coalescing prefilter
↓
Regenerative adsorption dryer
↓
Particulate afterfilter
↓
Dry-air receiver/distribution
↓
Point-of-use filtration where required
The exact receiver and filter positions depend on the equipment configuration and air-quality design.
Step 6: Monitor pressure dew point
A dew point sensor provides one of the most useful indicators of dryer performance.
A rising PDP can mean:
higher moisture loading
inadequate regeneration
valve leakage
or:
desiccant deterioration.
However, a faulty or poorly installed sensor can also produce misleading readings.
I verify the measurement before replacing components.
Step 7: Inspect the regeneration system
Regeneration is essential to sustained dryer performance.
For heatless dryers, I check:
purge-air supply
purge flow
tower switching
and:
exhaust operation.
For heated dryers, additional checks may include:
heater function
blower function
temperature control
and:
cooling cycle.
These checks must follow the manufacturer's procedures.
Step 8: Inspect valves and mufflers
A leaking switching valve can allow:
wet inlet air to bypass the drying process
or:
excess compressed air to escape.
A restricted exhaust muffler can interfere with regeneration.
Kaeser's dryer-maintenance guidance identifies valve problems, purge-cycle abnormalities, and downstream dust-filter condition as important maintenance checks.
Source: Kaeser — Air Dryer Maintenance.
Common high dew point problems
| Problem | Possible cause | What I investigate |
|---|---|---|
| PDP rises during peak production | Airflow exceeds corrected capacity | Actual flow and pressure |
| PDP rises in hot weather | Excessive inlet temperature | Aftercooler and cooling |
| PDP gradually deteriorates | Desiccant aging or contamination | Media and upstream filtration |
| PDP suddenly rises | Valve or regeneration failure | Controls, purge, switching |
| Purge consumption increases | Leaking or incorrect valve operation | Valve condition |
| Tower fails to regenerate | Insufficient purge or heat | Regeneration system |
| Excessive desiccant dust | Media deterioration | Desiccant and afterfilter |
| High pressure drop | Filter restriction or incorrect flow | Filters and dryer sizing |
| Unusual dew point readings | Sensor issue | Calibration and sampling |
Maintenance safety
Regenerative dryers contain pressurized vessels.
Heated systems may also contain:
high-temperature surfaces
and:
electrical equipment.
Maintenance must therefore follow the approved:
shutdown → isolation → depressurization → cooling → verification
procedure.
I do not open a pressure vessel, disconnect a pressurized line, or service a heater without controlling the relevant hazardous energy.
My insights: What is a regenerative adsorption dryer
A regenerative adsorption dryer is not simply a device that dries compressed air. It is a complete moisture-control system in which adsorption performance and regeneration efficiency must remain balanced.
A regenerative adsorption dryer continuously removes water vapor by alternating between desiccant adsorption and regeneration. Its key advantage is the ability to achieve very low pressure dew points, commonly −20°C or −40°C, with specialized systems capable of −70°C. I select it according to required air quality, net airflow, regeneration energy, and total operating cost.
My first insight: Regeneration is what makes continuous drying possible
Adsorption removes water vapor.
Regeneration restores the desiccant.
Both functions are essential.
If adsorption is working but regeneration is inadequate, the dryer will eventually produce wetter air.
This explains why I investigate the complete cycle instead of simply checking the desiccant condition.
My second insight: Dew point should determine the technology
I start with:
What PDP does the process actually need?
If the requirement is:
+3°C PDP
a refrigerated dryer may be sufficient.
If the requirement is:
−40°C PDP
regenerative adsorption drying becomes a strong option.
If the requirement is:
−70°C PDP
I verify that the specific dryer and desiccant configuration can achieve and sustain that target.
I do not buy a −70°C system merely because it is technically capable of producing drier air.
My third insight: Purge-air losses can dominate lifecycle cost
A heatless dryer can appear attractive because its mechanical design is relatively simple.
However, it may consume:
15%–20% of incoming compressed air
during regeneration.
The compressor must produce that air.
For a large continuous-duty plant, the associated electricity can become significant.
That is why I compare:
heatless + heated purge + blower purge + HOC
using annual energy consumption rather than initial price alone.
My fourth insight: Air-treatment equipment must be designed as one system
A regenerative dryer cannot solve every contamination problem.
It removes:
water vapor.
It does not automatically eliminate:
oil vapor
solid particles
or:
microbiological contamination.
I therefore design the system around:
moisture separation → prefiltration → adsorption drying → afterfiltration → final air quality.
If oil contaminates the desiccant, replacing only the dryer media without fixing the upstream cause can lead to repeated failure.
My fifth insight: My practical regenerative adsorption dryer selection checklist
When someone asks me “What is a regenerative adsorption dryer?”, I explain the working principle first and then use the following purchasing sequence.
1. Define the compressed-air application.
Instrumentation, food processing, electronics, pharmaceutical production, or outdoor piping?
2. Specify the required pressure dew point.
For example:
−20°C, −40°C, or −70°C.
3. Specify required delivered airflow.
Use net dry-air demand at the point of use.
4. Identify operating pressure.
Include minimum and normal conditions.
5. Measure dryer inlet temperature.
Do not rely only on ambient temperature.
6. Check compressor type.
Oil-injected or oil-free?
7. Select the regeneration technology.
Heatless, heated purge, blower purge, or heat of compression?
8. Calculate regeneration losses.
Check both compressed-air purge and electrical energy.
9. Verify desiccant protection.
Include separator, drains, and correct upstream filtration.
10. Confirm downstream filtration.
Protect equipment against desiccant dust where applicable.
11. Review dew point monitoring.
Prefer suitable alarms and demand-based control where justified.
12. Compare maintenance.
Include valves, filters, heaters, blowers, sensors, and desiccant replacement.
13. Calculate lifecycle cost.
Include purchase, installation, compressor energy, heater energy, filters, maintenance, and downtime.
My final selection guide
| Project requirement | Dryer I would investigate first |
|---|---|
| General factory air at +3°C PDP | Refrigerated dryer |
| Small low-dew-point application | Heatless regenerative adsorption dryer |
| Continuous industrial −40°C PDP | Heated purge or blower purge |
| Large air demand with high energy costs | Blower purge and other efficient regenerative designs |
| Compatible oil-free compressor with recoverable heat | Heat-of-compression dryer |
| Extremely low dew point near −70°C | Specifically rated adsorption system |
| Outdoor freezing conditions | Adsorption dryer sized for required PDP margin |
The key principle is:
Regenerative adsorption drying should be selected according to required moisture control and total regeneration cost.
My preferred engineering sequence is:
Air-quality requirement → net airflow → pressure → inlet temperature → regeneration technology → filtration → lifecycle cost
This produces a more reliable result than choosing the dryer simply by its nominal capacity or lowest purchase price.
Conclusion
A regenerative adsorption dryer uses reusable desiccant and repeated regeneration cycles to produce very dry compressed air. Choose it by dew point, airflow, regeneration method, and lifecycle cost.